Single Shaft Shredder Manufacturing Concerns to Consider
2026-10-23
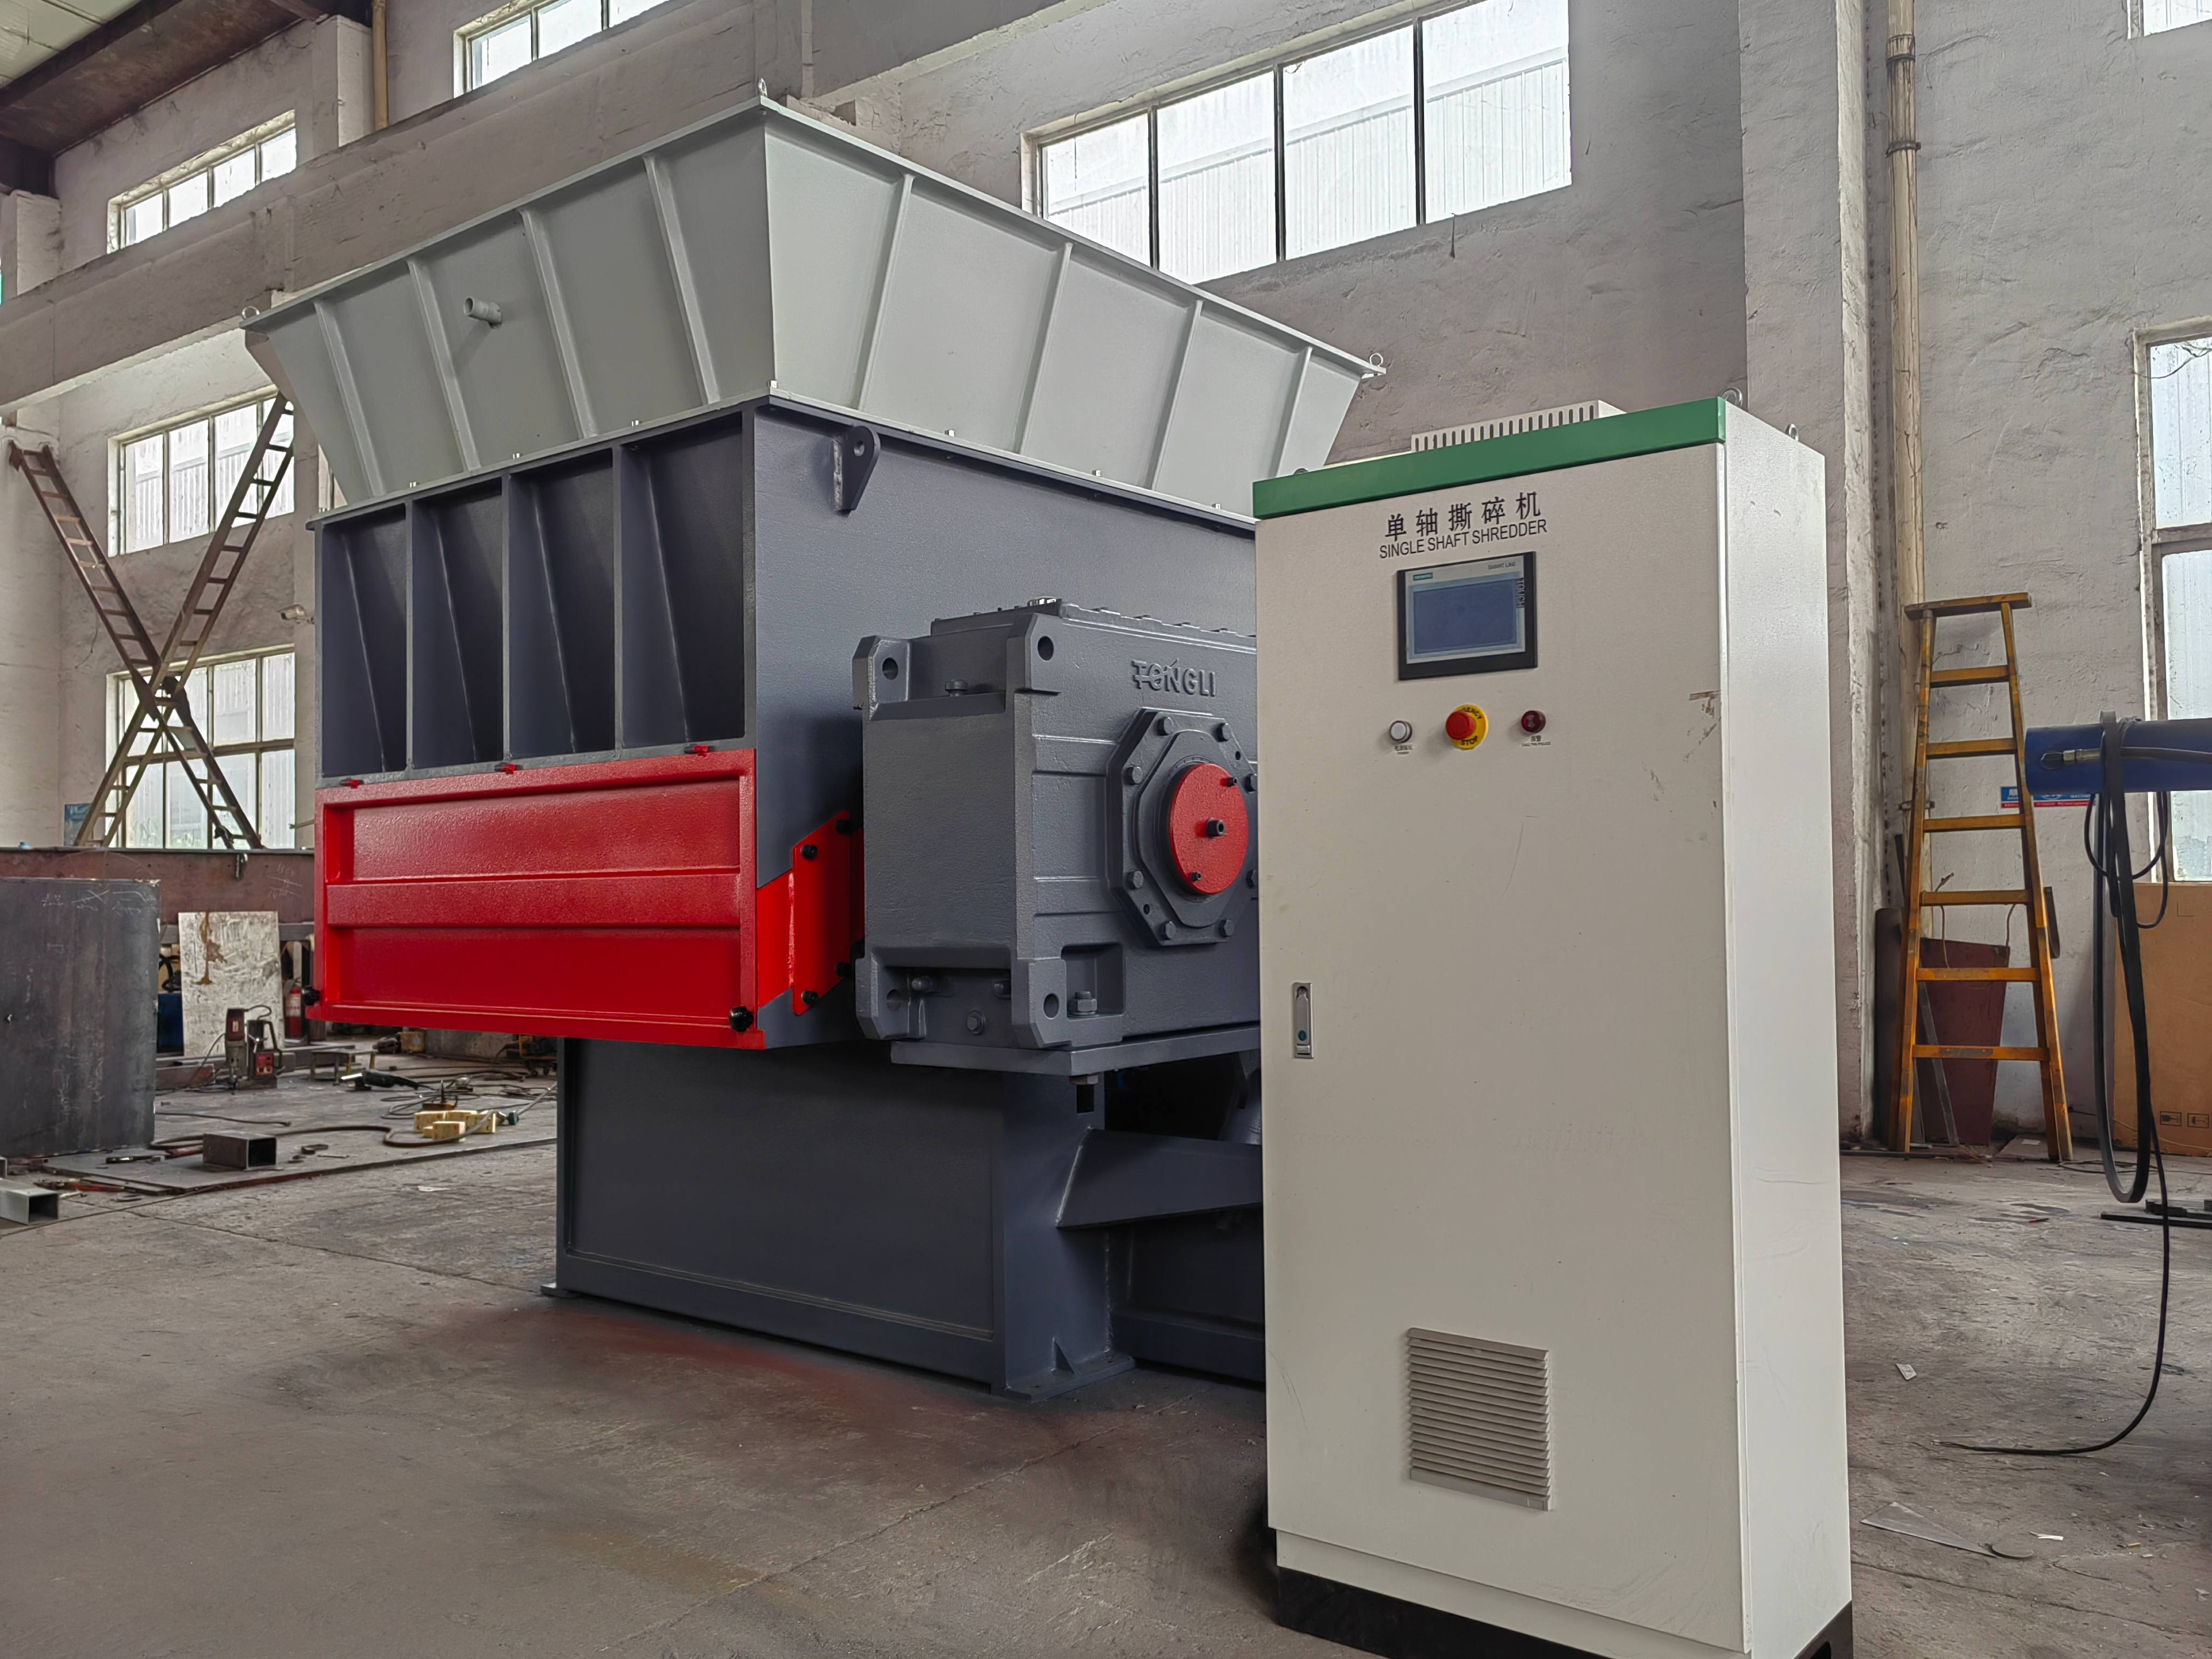
When sourcing a single shaft shredder, many buyers focus on cutting chamber size or motor power, yet the real performance hinges on manufacturing details that are rarely visible in a brochure. From rotor balancing tolerances to heat treatment of blades, subtle production choices determine whether your machine will chew through waste streams for years or become a maintenance headache within months. At Shengzhong Shredder, we've seen how overlooked concerns like bearing housing alignment and screen bar rigidity separate dependable shredders from costly disappointments. In this post, we'll unpack the manufacturing pitfalls you should question before committing to a purchase.
Rotor Balancing and Blade Alignment Tolerances That Keep Bearings Alive
Rotor imbalance sends destructive forces straight into the bearings. Even a few grams of unbalance at operating speed can create centrifugal loads far beyond what the bearing was designed to handle, leading to pitting, spalling, and premature fatigue. The goal is to keep balance tolerances tight enough to protect the bearings but still practical for field work.
Blade alignment matters just as much. When blades are not set at the same pitch or track, the rotor produces uneven thrust and vibration that hammer the bearing race. Measuring runout and adjusting each blade to within a few thousandths of an inch can double or even triple bearing life. Common balance grades like G2.5 work for many pumps and fans, but the real decision should come from the bearing manufacturer's limits and the actual shaft speed.
Tolerance stacking also plays a role. A rotor balanced on a mandrel may behave differently once assembled with couplings and keys. Final trim balancing on site, with blades aligned and all rotating parts fitted, is often the only way to keep residual unbalance low enough. Checking vibration at the bearing housing after final assembly and making small correction weights can keep a healthy bearing from becoming a monthly replacement item.
Knife Alloy Selection: Why Hardness Alone Leads to Chipping and Premature Wear
Many knifemakers chase high Rockwell numbers assuming better edge retention, but extreme hardness often backfires. In steels hardened to 64 HRC and above, the matrix becomes brittle and micro-chipping occurs under lateral stress or impact. A blade that measures impressively hard on a tester can still fail quickly in real kitchen use when it strikes a bone, frozen food, or a cutting board. This is because hardness reflects resistance to plastic deformation, not the ability to absorb energy without fracturing.
The real problem is carbide structure and grain size, not just hardness. High-alloy steels with large, clustered carbides may test hard but suffer from poor toughness. When the edge is thin, those carbide clusters act as stress risers. Under repeated loading, cracks initiate at the carbide-matrix boundaries and propagate, leading to visible chipping along the edge. A slightly lower hardness with a finer carbide distribution and finer grain often yields a more durable blade, even if the spec sheet looks less impressive.
Heat treatment also matters more than the hardness number. Over-austentizing or insufficient tempering can leave retained austenite or untempered martensite, both of which reduce edge stability. Multiple tempering cycles and cryogenic treatment can improve toughness without sacrificing usable hardness. The goal is a balanced matrix that deforms slightly under overload instead of snapping, so the edge rolls or dents rather than chips. This is why premium kitchen knives frequently sit in the 60–62 HRC range, not above it.
Bearing Seals That Survive Dust, Film, and Fine Particles Without Overheating
Dust and fine particles work their way under a seal lip and act like sandpaper on the shaft, while thin films from washdown or lubricant migration create a sticky, drag-heavy contact zone. Most sealing solutions solve one side of the problem—either they grip tight enough to block contamination but run hot, or they stay cool but let debris through. A seal that survives this environment has to manage both heat and exclusion at the same time.
The difference often comes down to lip material and shape. Compounds with low friction additives reduce running temperature without sacrificing flexibility, and a carefully designed lip angle keeps contact pressure low at the edge while still maintaining a sharp exclusion line. Adding a secondary wiper lip or a labyrinth-style outer barrier catches larger particles before they reach the primary seal, so the main lip only has to handle fine dust and residual film.
In practice, this means a bearing on a grain auger or a mining conveyor stays cooler after hours of running, even when surrounded by airborne chaff or metallic powder. The seals are not just surviving the dust—they are keeping heat buildup below the point where grease breaks down or shaft scoring begins. That is the practical test: after a full shift, the housing is warm but not hot, and the bearing is still clean inside.
Screen Open Area: Matching Perforation to Material to Avoid Motor Overload
Perforated screens with excessive open area can let too much material through at once, forcing the motor to work harder than intended. When the screen surface is too open for the material's bulk density and flow characteristics, the feed tends to surge rather than spread evenly. This creates a cycle of sudden load spikes followed by brief relief, which shortens motor life and can trip thermal overloads. Matching the perforation pattern to the material's particle size distribution and angle of repose helps keep the load steady.
Fine powders behave differently from chunky aggregates. A screen with large holes and thin ligaments might handle crushed stone without issue, but the same open area will cause dry sand or cement to flood through, overloading the drive. Reducing the hole diameter or increasing the ligament width lowers the open area percentage and restores resistance. In many cases, a layered approach works better: a top deck with smaller perforations to meter the flow, then a lower deck with larger openings for final sizing.
Operators often chase higher throughput by swapping in screens with more open area, only to find the motor drawing locked-rotor current on start-up. The real fix is testing a few perforation sizes under actual feed conditions. A screen that lets material pass slightly slower but keeps the amperage within the nameplate range will outlast one that runs hot every shift. If the material changes—say, from wet clay to dry pellets—the open area must be re-evaluated, because what worked before can become a motor killer after the switch.
Hydraulic Ram Force Settings: Fine-Tuning Pressure for Clean Cuts and Fewer Jams
Getting the ram force dialed in isn't about cranking the pressure to maximum and hoping for the best. Most jams and ragged edges come from operators treating the setting as a set-and-forget number. Instead, start with a baseline that's roughly 20 percent below the machine's rated capacity, then run a test piece and watch the cut line closely. A clean shear should sound like a smooth hiss, not a dull thud or a sharp crack. If you see tearing at the bottom of the stack or hear the pump laboring, back off a touch and retest.
One trick that rarely makes it into manuals is to adjust pressure in small increments while varying the material thickness. A setting that slices through 80-pound cardstock without a hitch might crush lightweight sheets or balk at laminated stock. Keep a simple log next to the machine—just a sticky note or a small notebook—where you jot down the gauge reading for each job. After a week, you'll spot patterns: certain fiber types need lower force but a slower ram speed, while coated papers want a sharper spike. This beats guessing every time and cuts down on stops to clear misfeeds.
Regular maintenance also plays a quiet role in keeping that fine-tuned pressure honest. Slight leaks in the hydraulic lines or worn seals can drop effective force by ten percent without tripping any warning light. If you notice the pressure drifting after a few hours or the cut quality degrading mid-run, check the fluid level and look for weeping around fittings. A five-minute inspection before a long shift often prevents the kind of cumulative drift that turns a good setting into a jam factory. Keep the adjustment knob clean, too—grit under the detent can make small changes feel sticky and unpredictable.
Stress Relieving the Frame: Preventing Cracks Under Constant Shock Loading
Residual stress from welding or machining doesn't show up on a drawing, but under repeated impact it becomes the crack initiation point. A frame that looks fine on a bench can fail early once shock loads start hammering the same joints. Stress relieving isn't just a heat-treatment checkbox; it redistributes locked-in tension so the material can flex without opening micro-tears.
For frames subjected to constant shock, the areas around gussets, bracket mounts, and abrupt section changes deserve the most attention. Stress concentrations there amplify the peak load far beyond the nominal stress. Vibratory stress relief can work well for large welded assemblies where furnace treatment isn't practical, while thermal stress relief remains the standard for critical sections. Either way, the goal is to knock down the residual tensile peaks before they team up with service loads.
After stress relieving, don't skip the verification. A quick check with X-ray diffraction or blind-hole drilling can confirm the residual stress dropped to an acceptable level. Then monitor the frame during the first hours of real shock loading—hairline cracks at weld toes or sharp corners are a sign that stress relief wasn't enough or that the design still needs a better load path. Catching those early is far cheaper than replacing a cracked frame in the field.
FAQ
Blade wear and breakage usually top the list, followed by main shaft fatigue if the rotor isn't balanced properly. Bearings can overheat when clearances are too tight or lubrication fails. Screen deformation happens when thickness is underestimated for the material type. Weld cracks in the frame also show up if stress relief was skipped.
It depends on the material stream. For general plastics and wood, D2 tool steel at 58-60 HRC works fine. If you expect tramp metal or abrasive fillers, DC53 offers better toughness without losing wear resistance. H13 is worth considering for high-temperature applications. Heat treatment consistency matters more than the alloy name, so specify tight hardness ranges and inspect for micro-cracks.
Even a few grams of imbalance at 80-120 RPM creates huge centrifugal forces that shorten bearing life and cause vibration cracks in the frame. We dynamically balance every rotor assembly after welding and before installing knives. Static balancing alone is not enough because the rotor is long and the mass distribution changes with each blade set.
The screen controls output size and also affects throughput. If the holes are too small, material backs up and overheats the cutting chamber. If the plate is too thin, it warps under pressure and rubs the rotor. We usually make screens from abrasion-resistant steel like Hardox and design them to slide out from the side for quick changes without dismantling the machine.
It is often overlooked but crucial. A welded frame with residual stress will twist after machining, throwing off the rotor alignment and blade gaps. We stress relieve the main frame after welding, then machine the bearing seats and screen rails in one setup. This keeps the rotor parallel to the screen and prevents uneven wear.
Hydraulic drives give excellent overload protection because they simply stall or reverse when jammed, but they run hot and waste energy. Electric motors with a gearbox are more efficient and quieter, but you need a reliable torque limiting system, like a fluid coupling or a vector drive with fast current limiting. For high-volume continuous use, we lean electric. For dirty mixed waste with frequent jams, hydraulic is more forgiving.
You cannot rely on standard lip seals alone. Shredder dust is fine and abrasive. We use a combination of labyrinth seals, grease purged cavities, and sometimes air purge ports on the bearing housings. The bearing housing itself should be split for easy inspection and the shaft should have a wear sleeve so you can replace the sealing surface without replacing the shaft.
At minimum, run the rotor up to full speed without load and check vibration levels on both bearing housings. Then feed some representative material if possible and monitor temperature and amp draw. Check the knife gaps with feeler gauges after the test and re-torque all fasteners. Also verify the hydraulic or electrical safety interlocks engage correctly under simulated jam conditions.
Conclusion
When building a single shaft shredder, the first concerns that separate a machine that lasts from one that needs constant bearing replacements are rotor balance and blade alignment. Even minor runout or misaligned knives create cyclic loads that hammer the bearings and shorten their life dramatically. Similarly, knife alloy selection is not about chasing the highest Rockwell number; overly hard edges are brittle and will chip when they hit tramp metal or dense material, so manufacturers need to balance hardness with impact toughness. The screen open area also cannot be an afterthought. If perforation size or pattern does not match the expected material feed, the motor will struggle against excessive backpressure and overload, which is a common field failure.
Beyond the cutting chamber, bearing seals must survive a harsh mix of dust, plastic film, and fine particles without generating excess heat. A seal that is too tight will overheat, while one that is too loose lets contamination in. Hydraulic ram force settings are equally critical; too much pressure forces the material into the rotor and causes jams or uneven cuts, while too little pressure reduces throughput. And the frame itself needs proper stress relieving after welding. Constant shock loading from the shredding process will find any residual stress and turn it into a fatigue crack, so skipping that step is a false economy.
Contact Us
Contact Person: Leon
Email: [email protected]
Tel/WhatsApp: 8615385558866
Website: https://www.shred-waste.com