Sintered Silicon Carbide Company: How to Choose a Trusted Supplier for High-Performance Components
2026-09-24
Sintered silicon carbide is only as good as the company that produces it. While many suppliers claim to offer high-performance components, few deliver the consistent quality and engineering support required for demanding applications. Before committing to a partnership, engineers and procurement teams must look beyond spec sheets and pricing. Factors like raw material sourcing, sintering process control, and post-machining precision separate dependable manufacturers from the rest. In this guide, we break down the key criteria for selecting a trusted supplier—and why HUAYI TECH has earned its reputation among industry professionals who refuse to compromise on performance.
Start with the Powder, Not the Polished Sales Pitch
If the first thing people see is a smooth pitch, they assume the product has been sanded down and staged. Starting with the powder means showing the unvarnished core: the raw ingredient list, the code before cleanup, the unretouched sample. It shifts the conversation from persuasion to inspection, and that is harder to fake.
Powder has texture. It clumps, it settles, it leaves traces. A polished sales pitch tries to remove all of that. But buyers have learned to distrust surfaces that are too clean. When you open with the powder, you invite friction: a detail that doesn't photograph well, a stat that complicates the story, a demo that shows a limitation. That friction is exactly what makes the rest of your message believable.
Put the glossy finish at the end, not the front. Use it to summarize what the powder already proved. The order matters more than the vocabulary. A pitch that begins with substance can afford to be elegant later; a pitch that begins with elegance often has nothing behind it.
Ask How the Sintering Curve Was Developed—Not Just the Peak Temperature
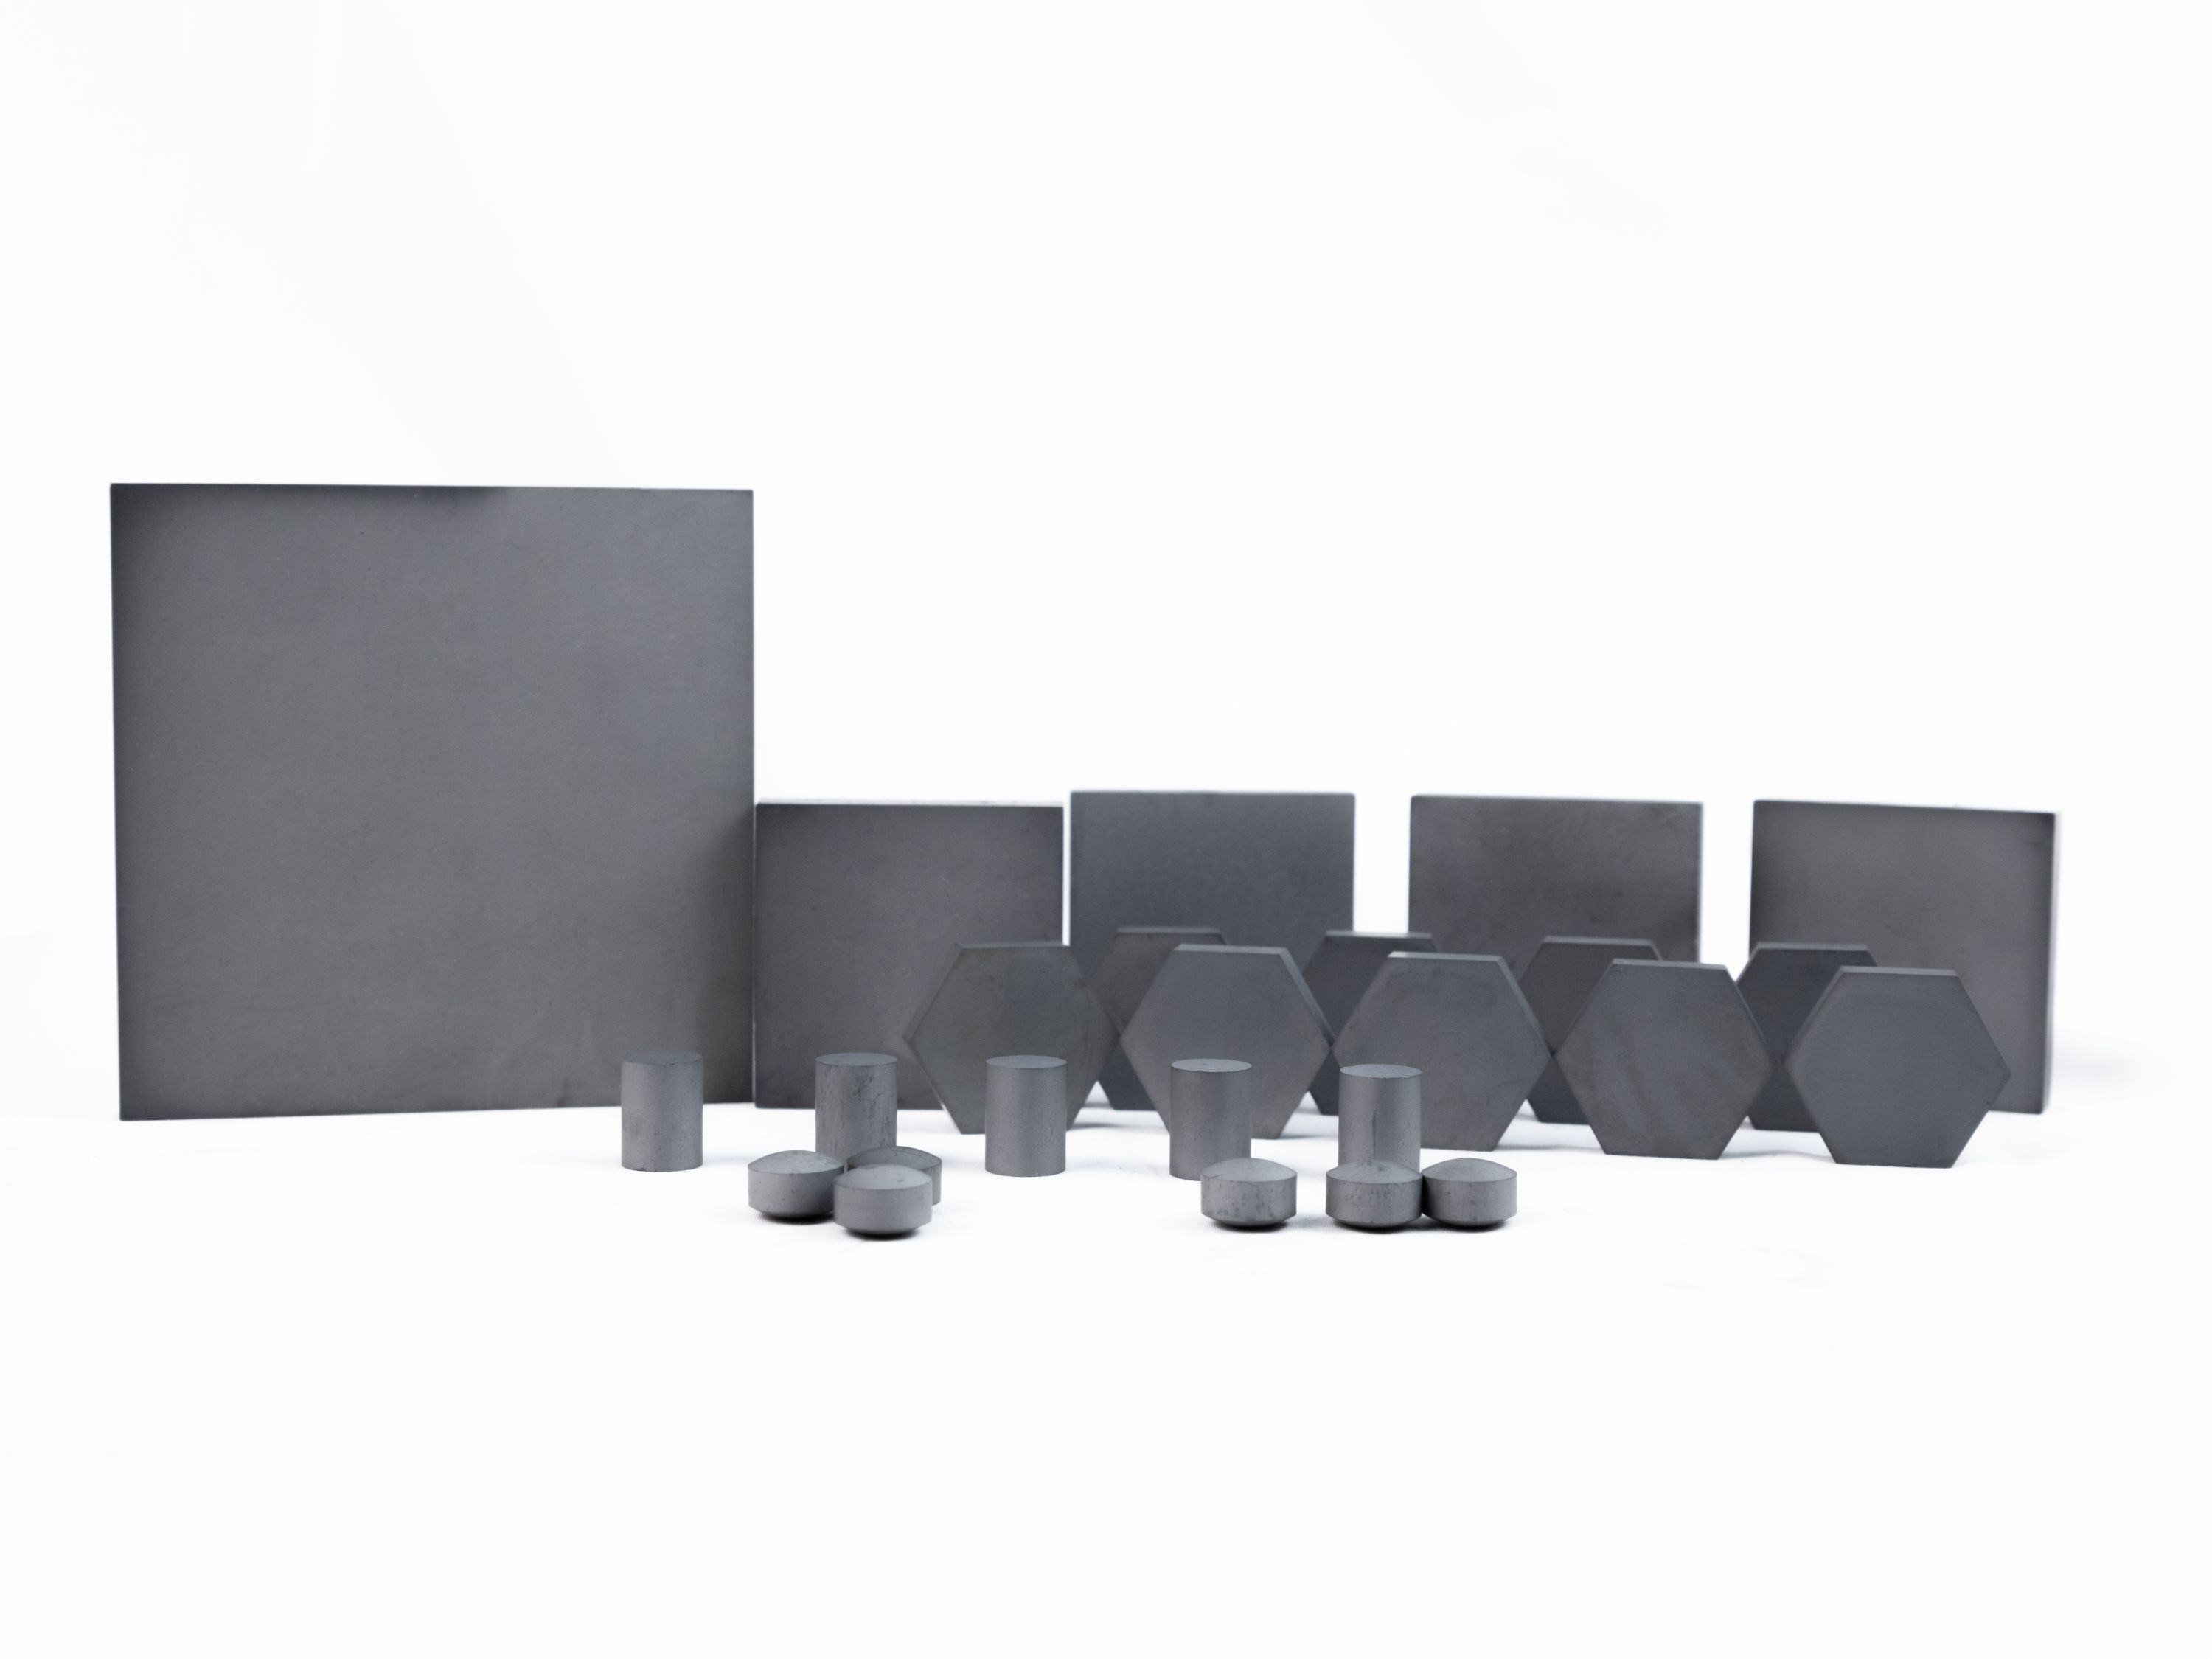
Most people fixate on the highest temperature a part will see, but that single number tells you almost nothing about whether the sintering profile actually fits the material. Ask instead how the entire curve was mapped: what the heating ramp looks like, where the deliberate holds are placed, and how fast the furnace is allowed to cool. A well-developed curve usually starts with thermal analysis of the green part, so binder burnout and any phase changes get their own controlled steps instead of being rushed through.
The holding time at peak temperature matters, but so does the path getting there. Uneven heating through a critical temperature range can cause warping or density gradients that no amount of peak soak will fix. A good sintering curve also accounts for the real thermal lag inside the furnace, not just the setpoint on a controller. If someone can explain why a specific ramp rate or intermediate dwell was chosen, that is a sign the profile was engineered for the part rather than copied from a generic chart.
Cooling is easy to overlook, yet it often controls grain size, residual stress, and even cracking in multi-phase materials. Ask whether the cooling rate was adjusted for the part's cross-section or if the furnace just shuts off and drifts down. The answer will quickly reveal whether you are getting a thoughtful process or only a peak temperature reading.
Request a Coupon Sample for Independent Testing Before You Commit
Before you commit to a bulk order, ask for a physical coupon sample. There is no better way to judge paper weight, coating, and print clarity than by holding the finished piece in your hands. A sample lets you check whether the barcode scans reliably, the perforations tear cleanly, and the colors match your brand standards under real lighting.
Independent testing also reveals how the coupon behaves in the field. Give the sample to a cashier, run it through a point-of-sale system, or let a few customers handle it. This step uncovers problems that digital proofs miss, such as smudging, curling, or poor adhesive on peel-off formats.
Treat the sample as a low-cost insurance policy. If something feels off, you can adjust the material or layout before production begins. A few days of testing now can prevent thousands of unusable coupons later.
Check for Batch Records That Show Consistency Over Time
Checking batch records over time is less about policing individual entries and more about spotting patterns that a single batch would never reveal. When you lay out three months of completed records side by side, small drifts in yield, cycle time, or even the frequency of manual adjustments start to stand out. Those drifts often mean something real is happening on the floor — a filter wearing out, a sensor losing calibration, or a new operator following slightly different steps. The batch record becomes a timeline, not just a checklist.
A practical way to do this is to pull the same ten or twelve fields from each batch — finished weight, critical processing temperatures, hold times, cleaning verification results — and plot them in sequence. Look for gradual trends as much as out-of-spec readings. A parameter that stays inside limits but moves a little every week may be a bigger risk than a one-off deviation that was caught and corrected. When records stay flat and predictable over several campaigns, that consistency is usually a sign that raw material handling, equipment settings, and operator training are all in sync.
It also helps to compare records around specific events, like a major maintenance shutdown or a change in raw material supplier. If the numbers before and after an event look statistically identical, the change was likely managed well. If they don't, that's your cue to investigate before the next lot ships. Consistency over time isn't just a nice-to-have for auditors; it's one of the few early signals you have that a process is still under control.
See How They Handle Design Changes Without Inflating Lead Times
A design tweak usually triggers a quiet panic in a machine shop: new toolpaths, recut fixtures, and a delivery date that slips before anyone says a word. One outfit I've watched handles it differently. Their CAM engineers work from a single revision-controlled model that links directly to the cutting queue. So when a hole moves or a pocket deepens, the change flows into the existing nesting plan instead of starting a separate job. The updated part goes on the same sheet as the original batch, and the lead time barely twitches.
That kind of speed comes from a simple rule: any change that doesn't alter the part's outer envelope or its critical datums gets processed without a formal design review. The shop floor can flag tolerance risks in real time, but minor adjustments—like adding a chamfer or shifting a non-critical slot—are treated as routine edits. It removes the back-and-forth emails and keeps the schedule honest instead of padded.
Weigh the Real Cost of a Lower-Priced Silicon Carbide Part
A lower sticker price on a silicon carbide part rarely tells the whole story. What looks like a straightforward saving often shifts cost into less visible places—shorter service intervals, unexpected thermal fatigue, or a failure that takes down an entire batch.
In high-wear or high-temperature settings, subtle differences in grain structure, sintering quality, and surface finish separate a part that lasts thousands of hours from one that degrades in weeks. A cheaper part may use recycled or inconsistently graded powder, leaving microvoids that become crack initiation points under cyclic stress.
The real cost shows up when you factor in labor for frequent replacements, lost production during unplanned downtime, and the risk of contaminating adjacent components. Paying more upfront for a tightly controlled SiC grade often reduces total cost per operating hour, even if the purchase order looks less attractive.
FAQ
It combines extreme hardness, high thermal conductivity, and excellent corrosion resistance, so parts hold up in abrasive or chemically aggressive environments where metals or standard ceramics fail.
Ask them to walk you through their sintering process, including powder preparation, pressing method, and firing temperature profile. A genuine manufacturer will discuss specific parameters like density targets and grain size control without hesitation.
Look for ISO 9001 as a baseline, but also ask about material test reports for each batch. Reputable suppliers will provide data on density, hardness, flexural strength, and porosity rather than just a generic certificate.
Sintered silicon carbide is notoriously difficult to machine, so find out whether they use diamond grinding, laser machining, or other specialized methods. Also ask about tolerances they can hold on complex geometries like seal faces or pump shafts.
Request samples from two or three separate production lots and have an independent lab test them. Compare the measured density and modulus of rupture across lots; tight scatter indicates solid process control.
It is critical. You want a supplier who can help with design modifications, failure analysis, and material selection for new applications. A supplier who disappears after delivery will cost you more in the long run.
Vague answers about sintering conditions, reluctance to share test data, inconsistent pricing without clear justification, or no references from companies in your industry. Also be wary of suppliers who promise unusually fast delivery for complex custom parts.
Conclusion
Selecting a sintered silicon carbide supplier requires looking past polished marketing and into the raw material story. A trustworthy partner starts with high-purity powder—its particle size distribution, impurity levels, and lot-to-lot consistency directly shape the final component's density, hardness, and wear resistance. Instead of accepting a glossy pitch, ask for the powder specification sheet and how they trace each batch back to its source. The sintering curve matters just as much as the peak temperature; a supplier that can explain the heating rate, hold times, and cooling profile—and how those were optimized for your geometry—demonstrates real process control. Request a coupon sample from the same production line, not a hand-picked demo part, and send it to an independent lab for density, flexural strength, and microstructure checks before committing to a volume order.
Beyond initial qualification, consistency is everything. Ask to see batch records spanning several months; look for tight control over density, hardness, and dimensional tolerance rather than occasional impressive numbers. When design changes arise, a responsive supplier will adjust tooling or sintering supports without inflating lead times or charging punitive fees—this reveals whether they have genuine engineering capacity or just a rigid production line. Weigh the real cost of a lower-priced silicon carbide part: a cheaper quote often hides looser tolerances, higher scrap rates, shorter service life, or hidden logistics costs. The true measure is cost per reliable operating hour, not price per piece. A supplier who earns your trust will be transparent about powder selection, sintering history, batch data, and design flexibility—ultimately delivering high-performance components that hold up where it counts.
Contact Us
Contact Person: Junting Leo
Email: [email protected]
Tel/WhatsApp: +86 18615009766
Website: https://www.huayimaterial-china.com/